
How to Machine G-10
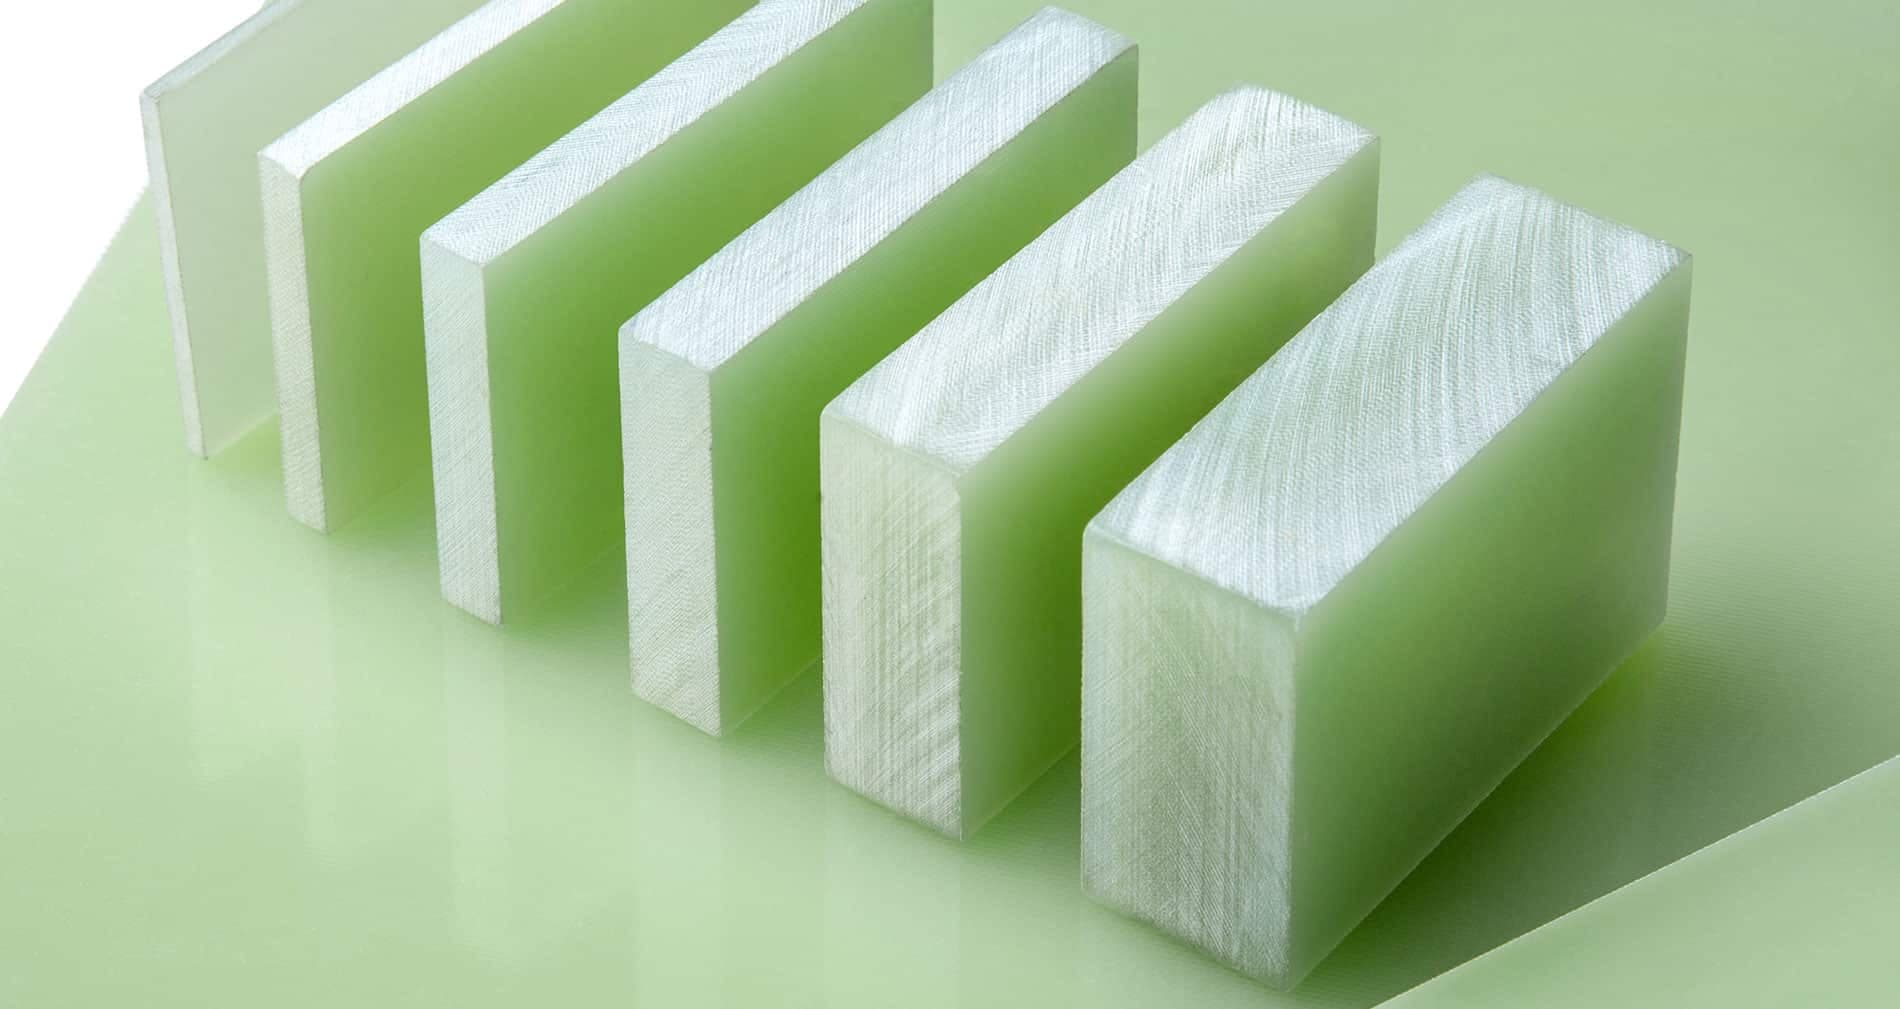
G-10 material (written G10 just as often, and sold by some distributors under the name Garolite) has been used across industry for decades and is still picking up steam. The properties that make G-10 so useful, woven glass cloth locked in a hard epoxy resin, are exactly what make it harder to machine than metals or softer plastics. Glass is abrasive, so it wears ordinary steel tools quickly, and if you machine G-10 with the same technique you would use on metal, you risk chipping and delamination. With the right tooling it machines cleanly: it can be cut on a CNC router or mill, by waterjet, or on saws and lathes, then finished into precise tool handles, knife scales and other parts. Diamond-coated and carbide tools work best. This guide covers the equipment and techniques, how to cut G10 by hand, and how to keep the dust under control.
Different Ways to Machine G-10
The best way to get into machining G-10 is to know each piece of equipment and the technique that suits your desired end product. Garolite machining follows the same rules whichever grade you use: G-10, FR-4 and the high-temperature G-11/FR-5 all cut the same way.
Circular Saw
Circular saws cut straight lines and work well on G-10/FR4 sheet. Use a diamond-impregnated wheel, and have a good exhaust system and dust filtration in place so the dust does not build up. Do not let the blade dwell in the cut: friction overheats the material and burns the edge. If overheating does occur, cool the work and the wheel with water.
Band Saw
A band saw is the quickest way to rough out shapes. For G-10 a carbide-tipped or carbide-grit blade is recommended, and as always you need a good system for handling dust. A standard steel blade will cut G10 but dulls very quickly.
Shearing
Shearing cuts unwanted material away from a larger sheet in one stroke. It can be used on G-10 up to 3/32″ thick; thicker sheet should be sawn or routed.
CNC Milling and Routing
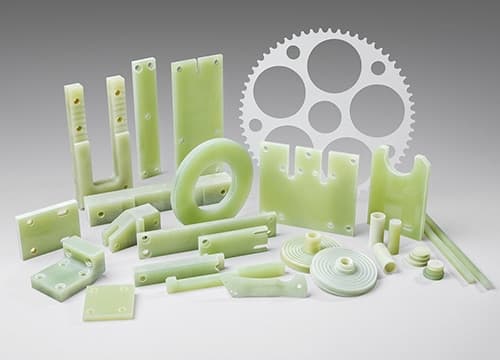
CNC is how most G10 parts are made, from knife scales to insulators and spacers. Any conventional metalworking mill or CNC router will do the job if it runs carbide or diamond (PCD) tooling. A few rules make the difference between a clean edge and a frayed one:
- Use sharp carbide or diamond-coated end mills. Compression cutters leave a clean top and bottom face on sheet.
- Run high spindle speeds with a steady feed, so the tool cuts rather than rubs. Rubbing generates heat and scorches the resin.
- Hold the sheet flat and tight, with a spoilboard or fixture under it, so the last ply does not break out when the tool exits.
- Collect dust at the cutter with a vacuum shroud or run a water-based coolant. Dry cutting without extraction fills the shop with glass dust.
Turning, Boring, and Facing
Turning, boring and facing shape G-10 rod and tube down to final dimensions on lathes, automatic screw machines and turret lathes. Use carbide-tipped or PCD tools; high-speed steel wears out within a few parts.
Drilling and Tapping
Drilling and tapping go hand in hand, since tapped holes start as drilled ones. Use a carbide drill; steel drills are only good for short runs. Back the sheet to prevent break-out on the exit side, and check the first hole, because laminates can close up slightly after drilling. G-10 taps the same way paper-based phenolics do.
Threading
Threading follows directly from drilling and tapping. As with every other operation, carbide-tipped tools give the best results, with fine, dry cuts.
Buffing
Grinding and sanding can be done on a belt, a disc or by hand; buffing then brings up the shine. For G-10, buff on a rag wheel. No lubrication is needed, but a buffing compound improves the finish.
How to Cut G10 by Hand
For a one-off knife scale or a small insulator you do not need a CNC machine. To cut G10 by hand:
- Mark the outline on the sheet and clamp it to the bench.
- Cut just outside the line with a hacksaw or coping saw fitted with a fine-tooth or carbide-grit blade. Let the blade do the work; forcing it chips the edge.
- File or sand down to the line. Wet sanding keeps the dust out of the air and gives a smoother edge.
- Drill holes with a carbide or cobalt bit at moderate speed, backed with scrap.
- Finish with progressively finer grits, then buff if you want a polished face.
Wear a respirator and eye protection even for hand work: the dust is fine glass and resin.
Personal Protection Equipment While Machining G-10
Machining G-10 is no different from any other shop work: stay as safe as possible and know what equipment you need.
- Eye protection. Small chips can fly off during any of the operations above. Goggles keep them out of your eyes.
- Gloves. Glass-fiber edges and dust irritate skin. Work gloves protect your hands when handling cut stock.
- Heat. Overheating can happen on any machine, not only saws. An overheated tool or part can burn someone who is not being careful, so keep coolant on hand.
- Dust extraction and a respirator. An exhaust system keeps the air clear of dust and fumes. When working with G-10/FR4, extraction and/or a respirator is essential: the dust from machining G-10 can be hazardous to breathe. The safety data sheet for your grade covers handling; ask us for it with your order.
Add any further measures your shop requires to keep you and everyone around you safe.
Current Can Help with Machining G-10 Today
Machining G-10 takes a little more care than other materials, but it is still machining. With carbide or diamond tooling, good dust control and some practice, it becomes routine. G-10 is used for a wide variety of purposes, from spacers and standoffs to knife handles, so learning to machine it pays off for many industries.
If you would rather receive finished parts, we machine G-10 to print in our own shop: custom fabrication covers CNC routing, turning, drilling and tapping from prototype to production. Send your drawing for a free quote.
G10 Machining FAQs
What is the best tooling for machining G10?
Carbide or diamond (PCD) tooling. G10 is glass-filled, so it wears high-speed steel very quickly; steel tools are only practical for a few holes or a short run.
Can you laser cut G10?
A laser will cut thin sheet, but it tends to char and discolor the edge of thicker stock, and the fumes need extraction. For profiles, CNC routing or waterjet cutting gives a cleaner edge.
Is G10 dust dangerous?
G10 dust is fine glass fiber and cured epoxy, and it should not be breathed. Use dust extraction at the tool, a respirator, eye protection and gloves, or cut wet to keep the dust down.
Is Garolite the same as G10?
Yes. Garolite is a trade name some distributors use for G-10 and FR-4 glass-epoxy laminate. It machines exactly the same way.
Why does G10 delaminate when I machine it?
Usually heat or a dull tool. A worn cutter rubs instead of cutting, heats the resin and pulls the layers apart, especially on the exit side. Use sharp carbide, keep the feed steady and back the sheet so the last layer is supported.